Cold Plate Cleanliness for AI Servers: What to Specify Before Delivery
Specify cold plate cleanliness as a delivery requirement, not just a cleaning instruction. The drawing and purchase agreement should identify which internal surfaces are assessed, how contamination is measured, what the buyer will accept and how that condition will be protected until assembly.
This is a separate question from thermal performance or leak tightness. A leak-test result does not measure residual particles, and a photograph of clean ports does not document the full internal flow path. For an AI server cold plate project, agree on the evidence needed before approving production parts—not after the first shipment arrives.
This guide covers component acceptance and handover. It is not a chemical-cleaning recipe or a commissioning procedure for an entire data center.
Define the Cleanliness Requirement Before Approving the Drawing
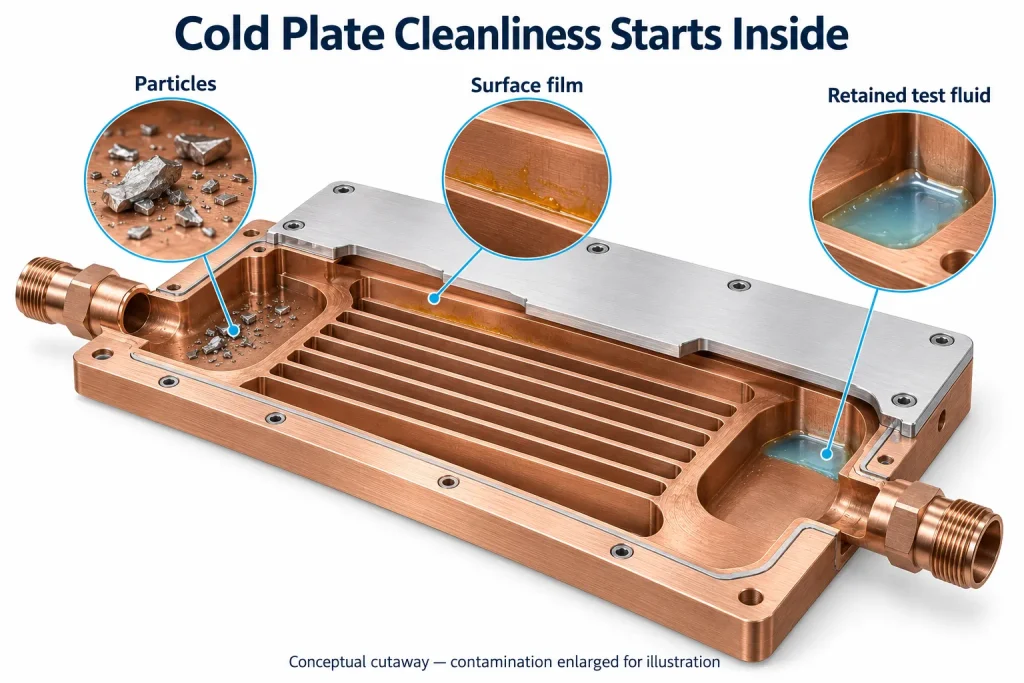
“Clean” alone cannot tell a supplier which surfaces matter, what contamination is being controlled or what evidence must accompany the shipment. Resolve those questions before approving the drawing so the purchase order and inspection plan describe the same deliverable.
Start with the inspection boundary. Identify the wetted internal channels, inlet and outlet ports, and any fittings supplied with the assembly. State whether removable fittings are included in the assessment. Treat external mounting surfaces as a separate requirement: an acceptable exterior does not establish the condition inside a coolant passage.
Also separate particulate contamination from films and chemical residues. A particle assessment does not, by itself, demonstrate the absence of oil or cleaning-agent residue. If these matter to the project, define separate acceptance criteria and evidence rather than expecting one particle report to cover everything.
| Requirement | What to agree |
|---|---|
| Contamination metric | The characteristic being measured, reporting unit and acceptance limit |
| Inspection method | The method and revision, applicable surfaces and agreed deviations |
| Sampling basis | Whether acceptance applies to each assembly, a production lot or a defined sample |
| Release conditions | The evidence required and the point at which the approved condition must be established |
ISO 16232:2018 addresses methods for determining and reporting particulate contamination on road-vehicle components. It does not establish component cleanliness limits or cover oil films and operating-fluid chemistry. Its use for a server project therefore needs an agreed scope; citing the standard alone does not create a complete acceptance specification.
Keep these requirements alongside the cold plate design brief, with the relevant specification referenced by the drawing and purchase order. Channel geometry and material selection describe the part to manufacture. The cleanliness specification describes the condition in which it must be delivered.
Make the Inspection Method Part of the Acceptance Criteria
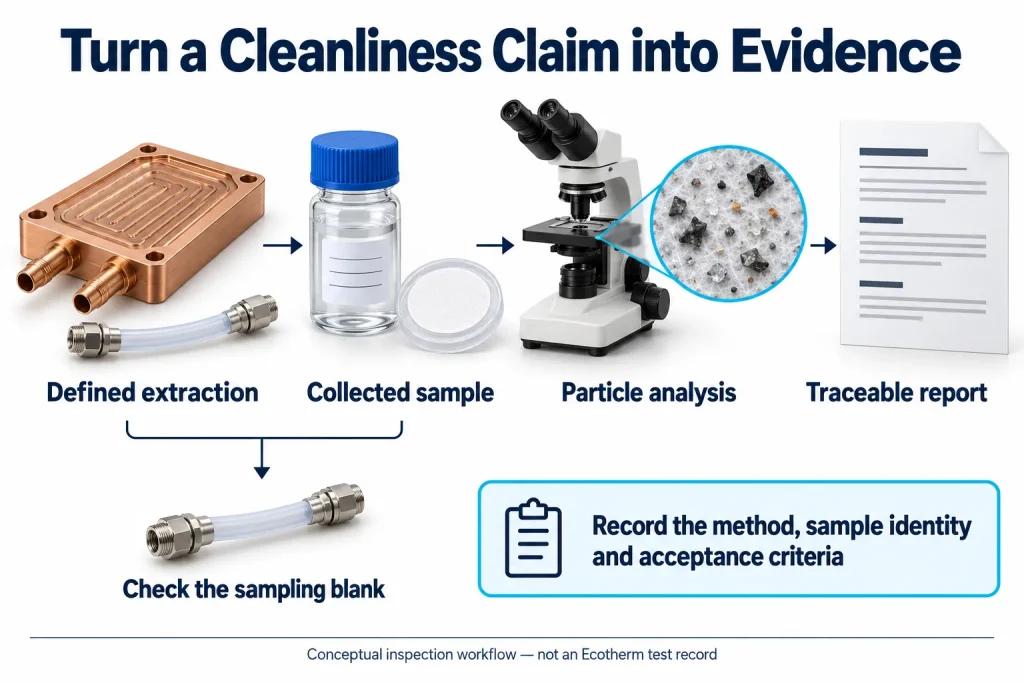
“Flushed” describes a manufacturing step; “pass” describes a decision. Neither tells a buyer how cold plate cleanliness was measured. Agree on a documented inspection method that another qualified operator can reproduce, including sampled surfaces, extraction conditions, analysis method and reporting basis.
Separate production cleaning from sampling extraction. Production cleaning prepares the part; extraction removes contamination for measurement. Evident’s washing-method overview describes collecting extracted particles in rinse fluid, filtering that fluid onto a membrane and using microscopy to assess particle counts, size distribution and characteristics. The extraction liquid must be compatible with the component, filtration equipment and membrane.
Ask the manufacturer and inspection provider to review the method for the actual assembly, including its passages, joints, seals and materials. Do not assume a cleaning or sampling technique suitable for an open metal component is suitable for a sealed assembly.
The procedure and report should identify:
– Part number, drawing revision, sample identity and lot, including whether results represent one plate or a pooled sample.
– Fluid identity and volume, flow direction, flow or pressure conditions, duration and collection boundary.
– Fixture configuration, membrane specification, analysis settings, blank reference and treatment of background contamination.
– Reporting units, normalization basis, acceptance limits and handling of invalid or failed tests.
The sampling setup can contribute particles of its own. Evident’s preparation workflow explains checking extraction-equipment background. It also notes that weighing collected residue does not reveal particle size or shape.
| Evidence | What it answers | What it does not prove |
|---|---|---|
| Visual port check | Is visible debris present at accessible openings? | Cleanliness throughout internal passages |
| Gravimetry | What residue mass was collected? | The largest particle’s dimensions |
| Membrane microscopy | What particles were extracted and measured? | All chemical contamination |
| Flow and pressure-drop test | Does hydraulic behavior meet the specified conditions? | Compliance with analytical cleanliness limits |
Hydraulic results can complement cleanliness evidence, but they measure a different property. Acceptable flow does not establish the amount or size of residual contamination.
Finally, define what happens to the tested part. Extraction changes its condition. Agree whether the sample is retained, reprocessed or eligible for delivery, and identify the approved steps needed to restore its required release condition after inspection.
Preserve the Approved Condition Through Shipment
Approval at an inspection station is not the end of cleanliness control. Review every operation between that inspection and the customer’s assembly process, including any later wet test, rework or reopened connection.
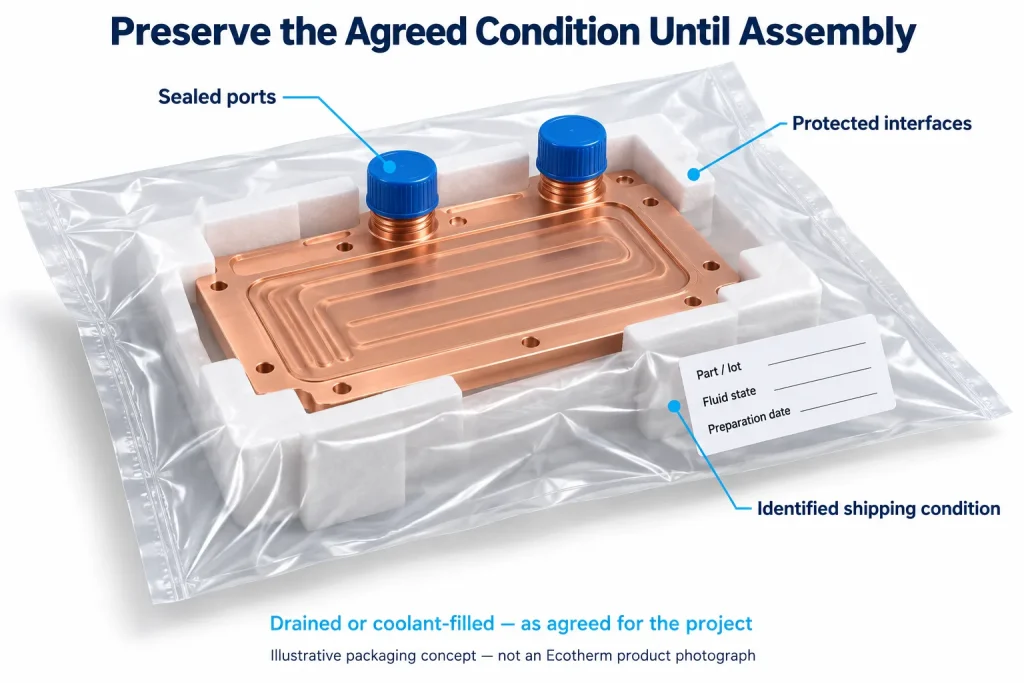
Section 3.2 of OCP’s Liquid Cooling Integration and Logistics White Paper describes cold plate preparation for transport. It addresses removing test fluid and particles, defining flushing conditions, controlling remaining moisture and sealing ports. It describes a drained preparation route and also allows coolant-filled shipment with the fluid identified. Choose the project’s approved route; “all plates must ship dry” is not a universal rule.
Before release, close these questions:
- What happens after the final check? Identify later operations that introduce fluid or expose channels. Define when they trigger cleaning and renewed verification.
- What fluid condition is acceptable? State the acceptance criterion and evidence for the agreed drained or filled state, considering storage duration and transit temperatures. Elapsed purge time alone does not establish dryness.
- How will ports remain protected? Specify clean, correctly fitting caps and protection for the interfaces. Keep packing materials away from exposed openings.
- What identifies the released condition? Link part and lot identification, drawing revision, fluid state, preparation date and storage conditions to the release record.
- What if protection is compromised? Define a receiving hold and engineering review for displaced caps, damaged seals or uncertain fluid history. Do not make unapproved flushing or adding cleaner the automatic response.
Have the supplier explain how the proposed packaging preserves the agreed condition through handling and unpacking. A protective bag is useful only as part of that plan; its presence is not proof of internal cleanliness.
Agree Who Owns Cleanliness at Each Handover
A cold plate accepted at the supplier can acquire contamination during assembly or site connection. Define who controls each stage, where acceptance occurs and what happens when a component is opened, modified or rejected.
OCP’s row manifold preparation guidance addresses pipework cleaning before connecting liquid-cooled racks and CDUs. It explains that debris and corrosion products can foul narrow cold plate passages. Its scope explicitly excludes rack and CDU commissioning, illustrating why the boundaries between these activities matter. Do not copy a row-piping cleaning procedure into a cold plate component specification.
Assign responsibilities explicitly:
| Handover | Agreement needed |
|---|---|
| Cold plate supplier to server integrator | Supplied assembly boundary, release evidence and receiving checks |
| Server integration and rework | Controls for installation, connector assembly, filling and reopening connections |
| Facility connection and commissioning | Site pipework readiness, approved connection sequence and the responsible equipment teams |
Use a handover record linking the part or batch, drawing revision, accepted scope, release report, receiving check and responsible owner. Record subsequent opening or rework and the disposition: accept, investigate or repeat an agreed verification. This creates a usable history if contamination appears downstream.
For an initial manufacturing enquiry, send an existing drawing or application layout, your contact details and any known customer cleanliness specification. You do not need a completed inspection plan to begin that conversation.
Before a firm production agreement, resolve the inspection boundary, acceptance method, coolant, port interfaces, shipping condition and quantities. Ask who will perform the proposed inspection and what report can actually be supplied. Keep unconfirmed requirements visible as open technical items in the quotation.
Planning an AI server cold plate? Share your drawing and available acceptance requirements through Ecotherm’s custom liquid cold plate page to discuss manufacturing feasibility and the inspection details that need confirmation before ordering.